Our 5-Step Factory Journey
From receiving bags of raw nuts at our factory gate in Igugu to nitrogen vacuum-sealing export cartons for buyers worldwide.
.jpeg)
Raw Nut Intake & Sun-Drying
When trucks bring raw cashew bags from our farmer partners, our team tests moisture levels and checks Kernel Outturn Ratio (KOR). The nuts are sun-dried on clean concrete aprons until moisture drops below 8% before moving into storage bays.
.jpeg)
Steam Cooking & Shell Conditioning
Raw nuts are fed into steam cookers to soften the tough outer shell and loosen the cashew nut shell liquid (CNSL). Steam conditioning makes cracking easier and helps preserve whole kernels inside.
.jpeg)
Mechanical Shelling & Borma Drying
Our mechanical shellers crack the outer shell with controlled pressure to extract intact kernels. The kernels then move into Borma drying ovens, where gentle heating shrinks the inner testa skin so it can be peeled cleanly.
.jpeg)
Peeling, Hand Grading & Size Sorting
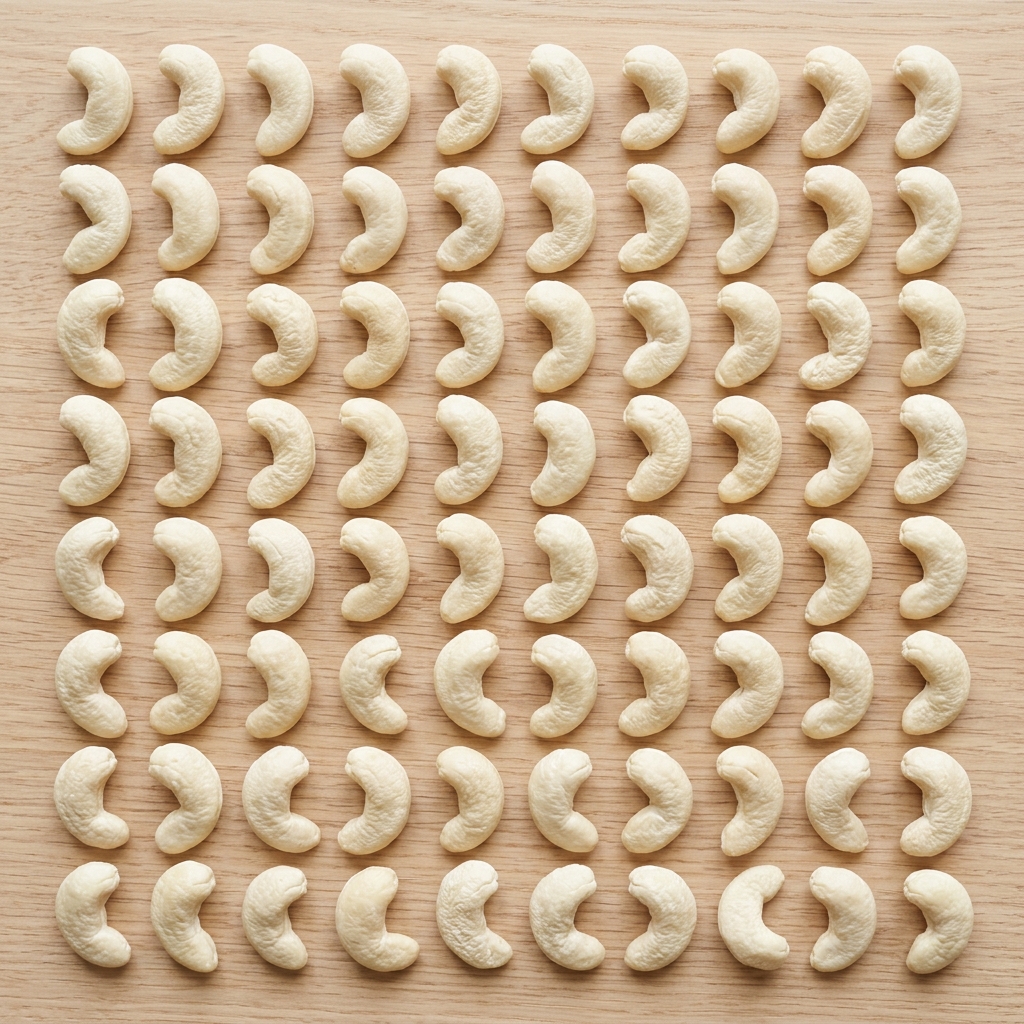
After peeling, our trained team hand-grades the kernels into standard international grades (such as WW240, WW320, splits, and pieces) based on size, color, and cleanliness, separating broken pieces for confectionery buyers.
Nitrogen Vacuum Packaging
Graded kernels are packed into heavy-duty poly-pouches, flushed with food-grade nitrogen gas, and vacuum-sealed. The pouches are packed in 22.68kg export cartons to maintain crispness and fresh taste throughout ocean shipping.
Uncompromising Quality Assurance
Our facility operates under strict NAFDAC health regulations. Every batch undergoes rigorous quality assurance testing before it receives its final export certification.